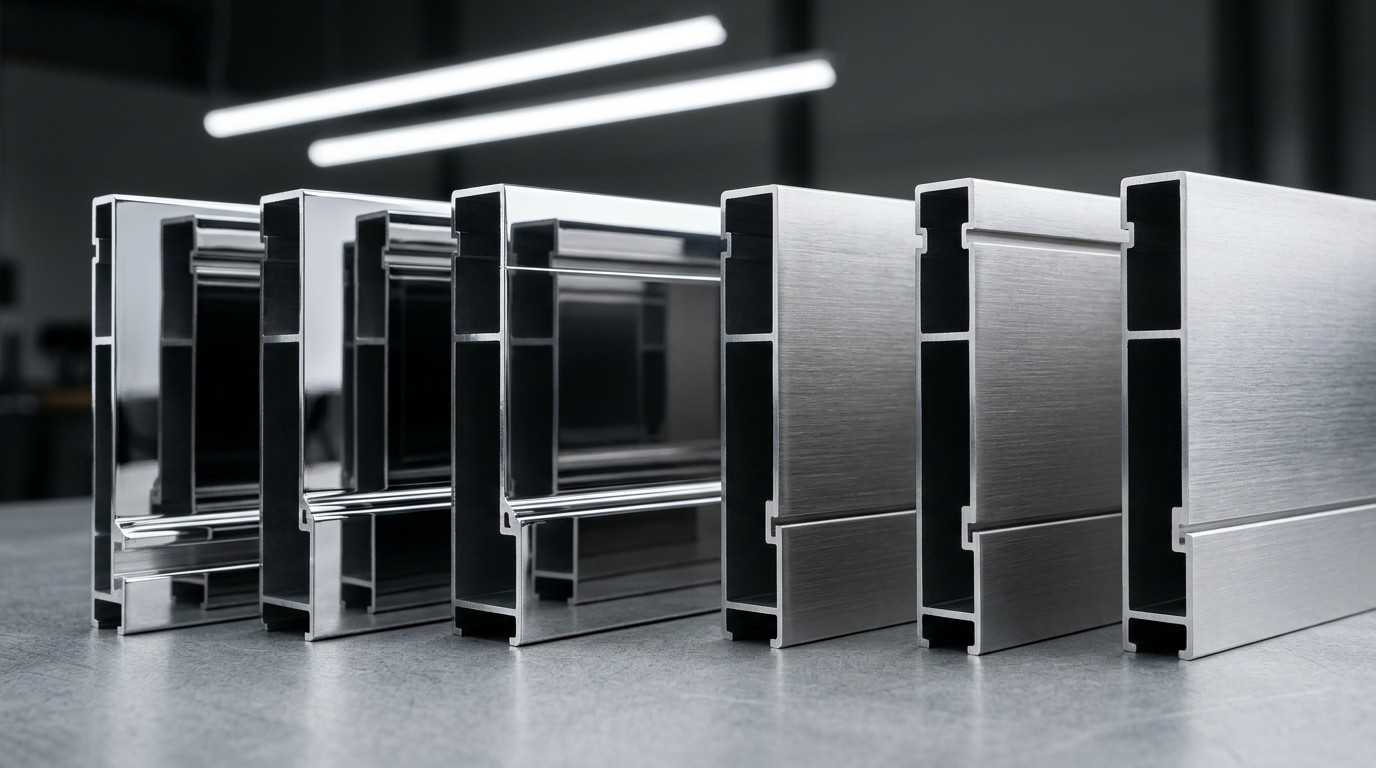
Special Surface Finishes
Mill finish, mechanical polishing, brushing (satin), sandblasting, small-part anodizing, and small-part powder coating planned within a single production flow.
Mechanical Polishing (E3), Satin Brushing (E2) and Chemical Etching (E6)
In architectural and decorative aluminium profiles, visual depth is defined by the pre-treatment performed before anodizing. On our mechanical polishing (E3) line, EN AW-6463 extrusions are buffed to a mirror-bright specular finish.
Satin brushing (E2) imparts a directional, silky grain resembling brushed stainless steel, while alkaline chemical etching (E6) removes light die lines to produce a uniform, non-reflective architectural matt surface.
Combined Texture and Anodized Color Depth
Polished (E3) and brushed (E2) textures can be combined with silver, gold, champagne, bronze or black anodizing to achieve durable metallic finishes for interiors and consumer products.
| Surface Finish | DIN 17611 Code | Recommended Alloy | Typical Applications |
|---|---|---|---|
| Mechanical Mirror Polishing | E3 | EN AW-6463 / EN AW-6063 | Shower enclosures, luxury retail displays and lighting reflectors |
| Mechanical Satin Brushing (Inox) | E2 | EN AW-6060 / EN AW-6063 | Kitchen/furniture handles, skirting boards and appliance trim |
| Polishing + Chemical Brightening | E5 | EN AW-6463 | Automotive decorative trim and high-gloss frames |
| Alkaline Satin Etching (Velvet Matt) | E6 | EN AW-6060 / EN AW-6063 | Curtain walls, windows, louvers and office partitions |
| Fine-Texture & Metallic Powder | RAL Effect | All 6xxx Series | Architectural accents and designer furniture structures |
FAQ
Is anodizing required after mechanical mirror polishing?
Yes. Unprotected polished aluminium oxidizes and dulls in air; applying clear or colored anodizing after E3 polishing permanently seals the mirror gloss.
How do you achieve a brushed stainless-steel (Inox) appearance on aluminium?
Profiles undergo E2 mechanical abrasive brushing to create a uniform linear grain, followed by natural silver or light champagne anodizing.
How do you control color consistency across production batches?
We establish signed physical master and limit samples with the client and lock billet chemistry, etching parameters and bath current density.
Related Engineering & Manufacturing Resources

5000, 6000 & 7000 Series Alloys (EN 573-3 / EN 755-2)
Chemical composition and mechanical property tables for EN AW-5083, 5754, 6060, 6063, 6005A, 6082, 6463, 7020 and 7075.
Read more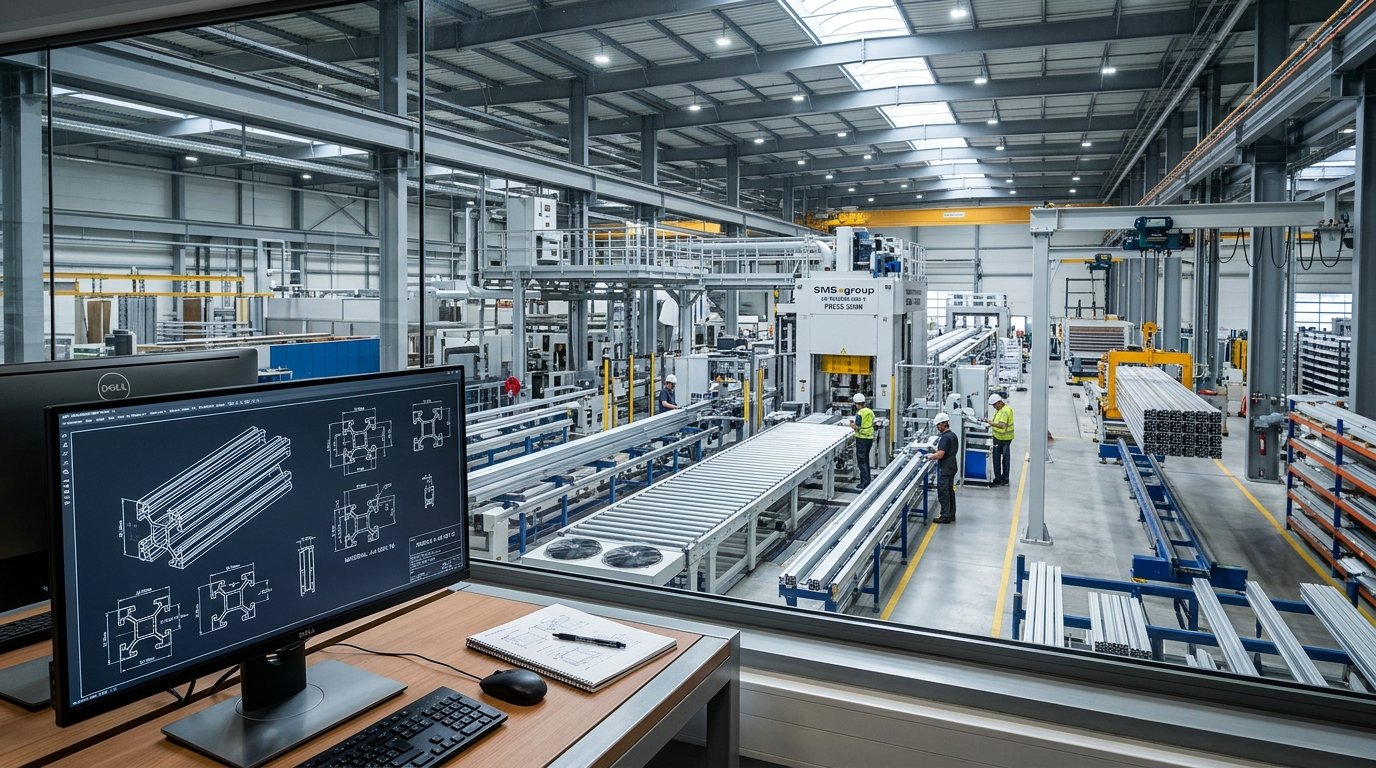
Plant, 5-6-7 Inch Presses & Small-Part Finishing
5-6-7 inch (1,000–2,000 t) presses, 80–20,000 g/m, min. 0.8 mm wall, bar/small-part anodizing & 8–6,000 mm cutting.
Read more
ISO 9001, TSE & 1-to-1 Replacement Guarantee
ISO 9001 and TSE certified quality control stages and 1-to-1 defect replacement commitment.
Read more
Request a Quote
Send your section drawing and annual volume; the quotation is prepared together with the die and production plan.